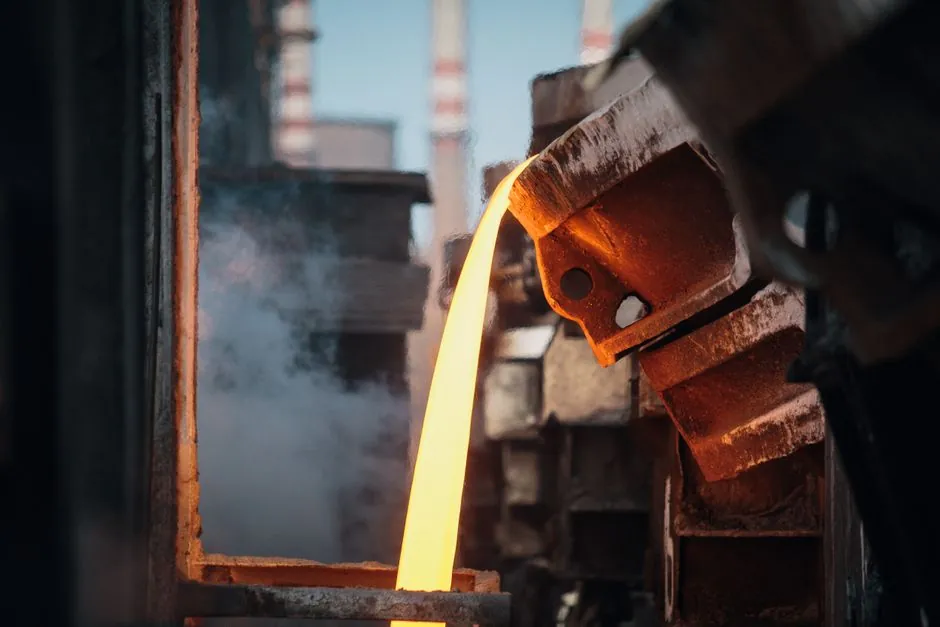
Compact induction melting units in the 50–500 kg capacity range, paired with medium-frequency IGBT power supplies drawing roughly 625 kWh per ton of steel melted, cover the bulk of telecom-enclosure aluminum and stainless feedstock requirements for tier-2 and tier-3 cabinet lines [S8].
Mains-frequency coreless induction furnaces are documented from sub-kilogram bench units up to 100 t steel-melt vessels, with 20 t and 10 t mains-frequency furnaces commonly grouped three-and-two on a single plant supply bus [S1][S6].
Frequency class, coil geometry, and enclosure-relevant capacity bands
Mains-frequency (50/60 Hz) coreless furnaces dominate the 5–100 t steel-melt band, with 80 t units cited as the upper commercial size in published plant references [S1]. For telecom-enclosure work the relevant size sits at the opposite end: medium-frequency (MF, typically 1–10 kHz) coreless furnaces in the 50–500 kg aluminum or stainless band, where melt rates of 0.5–2 t/h align with shift-wise cabinet batch output [S4].
MF units are built around three sub-assemblies: a medium-frequency power supply cabinet, a compensation capacitor cabinet, and the furnace body itself, with cold-pressed copper-strand water-cooled cables linking the coil to the bus [S4]. Heavy-walled, high-conductivity copper tubing is the standard coil conductor for maximum electrical efficiency on commercial melting units [S5].
Power-cabinet to furnace-body configurations and uptime behavior
Three published configuration patterns cover almost every telecom-enclosure fab layout: one power cabinet to one furnace body (lowest capex, no redundancy); one cabinet to two bodies with one cold spare (best balance of cost and uptime for two-shift operations); and one cabinet to two bodies both live, one fixed for smelting and the other for holding at pour temperature, which is the right pattern when long pour times or transfer-ladle cycles interrupt the melt schedule [S3].
For enclosure lines feeding die-cast or sand-cast aluminum housings, the dual-live pattern is the dominant choice because holding at 680–720 °C between pours is the rate-limiting step, not raw melt rate [S3]. The spare-body pattern is favored where downtime cost is dominated by unscheduled coil or lining failure rather than melt throughput [S3].
Energy budget, refractory, and cooling-water demand
The 625 kWh/ton rule of thumb for steel-melt induction furnaces is the baseline for sizing incoming power, capacitor banks, and switchgear, and it scales roughly with specific heat of the charge plus 5–10% coil-and-lining losses for ferrous melts [S8]. Non-ferrous melts of aluminum and copper run closer to 500–600 kWh/ton because of lower melt temperatures and better electrical coupling at medium frequency [S4][S8].
Refractory selection follows the charge: acid, neutral, and alkaline linings are the three published families for induction furnace crucibles, and the wrong pH class against a manganese- or sulfur-bearing stainless charge will cut lining life from a typical 200–400 heats to under 100 [S3]. Medium-frequency coreless furnaces in this size class also require a closed-loop cooling tower sized for roughly 8–15 L/min per 100 kW of coil power dissipated as heat, plus an SCR or IGBT-grade deionized water loop for the power cabinet heat-sinks [S4][S5].
Protection, controls, and commissioning gates
MF power cabinets in this class ship with multi-level protection: water pressure, phase loss, undervoltage, overcurrent, overvoltage, off-time, direct-pass DC bus, and operation interlock, and zero-voltage soft-start is quoted at 100% start success on parallel-inverter fifth-generation controllers [S4]. Inverter conversion efficiency for units operating at 1000 Hz and below is published above 96%, which is the figure procurement specs typically anchor to [S4].
Commissioning practice on a new MF furnace follows a defined sequence: mechanical leveling of the furnace body, hydraulic or gear-tilt verification, water-circuit leak test at 1.5x working pressure, coil megger and Hi-Pot, refractory bake-out on a staged ramp to roughly 900 °C over 24–36 hours, and a first-melt iron or aluminum pad to season the lining before production tonnage starts [S7]. Skipping the bake-out or shortening the pad-melt is the single most common cause of premature lining failure on small coreless units [S7].
Comparison of induction furnace classes for enclosure work
On four procurement criteria, mains-frequency coreless, medium-frequency coreless, and high-frequency compact units line up as follows: capacity (mains: 5–100 t; MF: 50 kg–10 t; HF: sub-50 kg, typically bench or tabletop); melt rate per kW installed (mains: ~0.8 t/h per MW on steel; MF: ~1.0–1.2 t/h per MW on steel and ~1.5 t/h per MW on aluminum; HF: limited to small precious-metal and lab use); specific energy (steel ~625 kWh/t; aluminum ~500 kWh/t; copper ~400 kWh/t) [S1][S4][S5][S6][S8].
Footprint and refractory cost favor MF for sub-5 t enclosure work, while mains-frequency wins only above about 10 t where capital cost per ton of installed melt capacity drops sharply [S1][S6]. For most telecom-enclosure fabs running 1–10 t of aluminum per shift, the MF coreless is the lowest total-cost-of-ownership option, and the related Cold Chamber Die Casting Machine Lifespan and Replacement Guide covers the downstream casting-side decisions that drive furnace sizing on the melt side.
Selection criteria and who should NOT buy a coreless induction furnace
Choose a coreless MF induction furnace when the charge is steel, stainless, iron, aluminum, copper, brass, lead, or zinc in the 50 kg–10 t batch range, when electromagnetic stirring is desired for chemical homogeneity, and when shop power can supply at least 300 kW per 500 kg of installed melt capacity [S4][S6]. Do NOT choose a coreless unit when the process requires vacuum or controlled-atmosphere melting (use a vacuum induction furnace instead), when continuous feed and discharge are needed (use a channel or holding furnace configuration), or when the charge is highly reactive titanium or magnesium, which demands a different crucible and atmosphere strategy entirely [S6].
For shops evaluating alternative thermal equipment for comparison, the crucible furnace class covers gas- or oil-fired batch melting at lower capex but higher emissions, and the broader melting furnace category frames the spec-driven choice between fuel-fired, resistance, and induction topologies. Plants weighing cupola replacement or scrap-iron charge workflows should review the cupola furnace reference for the cost-and-throughput trade-offs before committing to induction retrofit.
Trackable signals for the next planning cycle: published updates to MF IGBT controller firmware generations, refractory lining-life data from sub-1 t aluminum-melt installations, and any new efficiency benchmarks above the 96% inverter conversion mark at 1000 Hz and below [S4][S5]. Related heat treatment furnace and induction furnace reference pages cover the post-melt thermal-processing side of the same enclosure production line.