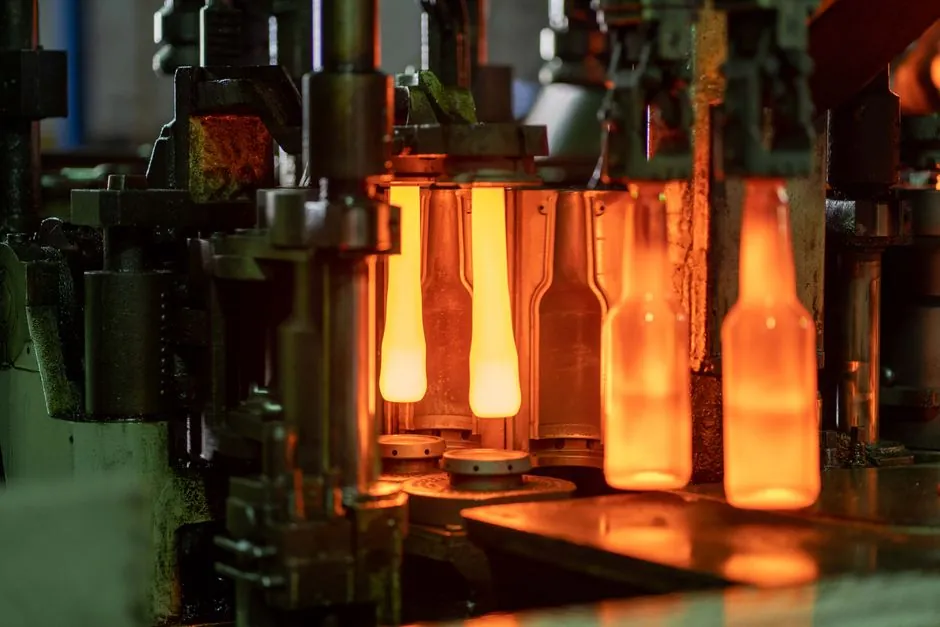
An automatic molding line swapping between two pattern sets on a conventional matchplate or horizontal flask cell still loses 30-90 minutes per transition before SMED is applied, with internal tasks (those requiring the machine stopped) making up roughly 60-80% of that window [S1][S2][S4].
Foundries running high-mix, low-volume work treat pattern-set changeover as a tracked OEE loss, not a setup nuisance, because every minute of stop-the-clock time multiplies across cells and shifts; the 2025 MDPI study on automotive injection changeovers quantifies similar drag in plastic molding, where plate-change and machine-idle time dominate the Manufacturing Cycle Time (MCT) [S5].
What pattern-set changeover actually clocks
Changeover time, defined as the gap between the last good part of one run and the first good part of the next, is broader than setup time: it includes preparation, idle/change, and post-production verification, with operators often conflating the two in shop-floor logs [S1][S2]. For an automatic molding line, that translates into pattern removal, blow-plate or stripper checks, flask or matchplate swap, sand-system parameter reset, and a short first-mold verification cycle.
The 10-minute target band that lean guides keep repeating is not arbitrary: it is the Single-Minute Exchange of Die (SMED) ceiling, where "single-digit minutes" means under 10 minutes, not under an hour [S1][S6]. A shop running an automatic level matchplate or core machine without SMED discipline will usually report changeover between 45 and 90 minutes; the same line, after a 3-6 month SMED project, drops into the 7-15 minute range for the same pattern swap [S1][S6][S9].
Where the minutes go: internal vs external task split
SMED starts by splitting changeover into internal tasks (machine must be stopped: removing the worn pattern, loosening clamps, resetting blow pressure) and external tasks (can be done while the line still runs: preheating the next pattern, staging clamps, verifying the next sand mix) [S1][S2]. On molding cells, internal work commonly accounts for 60-80% of total changeover minutes, which is why a naive "speed it up" effort stalls and a structural task-split delivers the gain [S1][S6].
The 2025 MDPI automotive injection study confirms the same shape in plastic: Value Stream Mapping plus time-motion analysis isolated plate-change and machine-idle blocks as the dominant MCT contributors, and shifting setup steps from internal to external was the lever that moved the number [S5]. For a molding line doing pattern swaps, the practical analogs are: pre-staged quick-clamp fixtures, pattern-specific parameter presets, and pre-aligned blow plates that can be carried to the cell as a unit.
Technique matrix: what actually cuts changeover time
Across the 2024-2026 sources, the recurring SMED levers on molding cells are: standardized changeover procedures with digital SOPs (cuts variation between shifts), pre-staged tooling and quick-release clamps (cuts internal minutes), pattern-specific recipe storage in the HMI or PLC (cuts adjustment and trial time), and parallel-operator work during the short internal window [S1][S3][S4][S7].
A 2025 EMI field note on pattern adaptability in molding machines adds two hardware-side levers that matter on real shell molding machine cells: regular calibration of blow plates and strippers (a 1 mm misalignment ruins the first molds and forces a re-do), and upgraded controls that recall pattern-specific presets instead of forcing manual re-entry [S4]. The same source flags machine-class differences: high-production core machines change patterns slowest unless retrofit, dual-station core machines change fastest in the medium-batch band, and manual machines are operator-skill-bound [S4].
Side-by-side: machine class vs changeover behavior
Decision criteria for matching machine class to pattern-change frequency follow a consistent pattern across the 2024-2026 sources. High-production core machines favor repeat jobs and long runs, where pattern-swap downtime is amortized over many molds, but suffer the longest changeovers (often 60-120 minutes) when patterns do change unless retrofitted for SMED [S4]. Dual-station core machines are the workhorse for medium-scale foundries doing frequent pattern changes: one station runs while the other is re-set, dropping effective changeover to a small single-digit number of minutes [S4]. Manual molding machines give the operator maximum control, but changeover time becomes a function of training and shift-to-shift consistency rather than a hardware number [S4][S9].
For a molding cell, the practical selection rule: pick a dual-station core machine when pattern changes exceed two per shift, stay on a high-production core machine when pattern changes are below one per shift, and use manual setups only for prototyping or very low repeatability jobs where changeover is not the gating loss [S4][S9]. A 2026 EAS change-systems write-up reinforces the magnitude: most manufacturers with no SMED program can compress changeover from hours to minutes (commonly 70-85% reduction) through planning, training, and quick-clamp hardware alone [S9].
Who this is for, and where SMED stalls
SMED-style changeover reduction pays back fastest on cells doing more than one pattern change per shift, on lines already instrumented with OEE or downtime tracking, and on shops that can hold operators on a standardized procedure across shifts [S1][S3][S7]. It pays back slowly or not at all on dedicated high-volume cells that change patterns less than once a week, where the engineering time spent on quick-clamps and presets dwarfs the recovered minutes [S4][S9].
The recurring failure modes are: operator-dependent adjustments that never get written down, handwritten settings that do not survive shift handover, calibration drift on blow plates and strippers that ruins the first molds after every change, and "one-off" changeovers that destroy the baseline [S1][S4][S7]. The 2026 MaintainX guide is explicit that without an execution framework (a written SOP, a clock start/stop rule, and a recorded first-good-part time) the SMED gain evaporates within a quarter [S7]. Related process-engineering work on adjacent casting decisions, such as the volume crossover between die casting and sand or investment casting, follows the same logic: the right choice depends on how often you change the pattern, not just on the per-part cost, which is why foundries revisit both choices together.
Measurement: the formula shops actually run
The 2025 First Resonance write-up gives the formula discrete manufacturers use in practice: Total Changeover Time = Downtime + Adjustment Time + Testing Time, where downtime is the line fully stopped, adjustment time covers physical part/tool swaps and settings, and testing time is the first-good-part verification [S3].
Two operational rules from the 2024-2026 source set that matter for molding cells: clock starts at the last good part of the previous run (not at machine stop) and stops at the first good part of the next run, and "good" is the customer's quality specification, not the operator's first-shot judgment [S1][S3]. A 2025 Tulip analysis notes that changeover is classified as "Waiting" in the eight lean wastes, which is why a stop-the-clock minute and an idle-waiting minute are not the same line item in an OEE rollup [S1].
Standards and sourcing that anchor the numbers
SMED itself is a lean methodology (Shigeo Shingo, Toyota) rather than an ISO or ASTM standard, so published targets like the under-10-minute benchmark are convention, not regulated thresholds; verification of a foundry's own number still requires a documented clock-start/clock-stop rule and a maintained changeover log [S1][S6]. The 2025 MDPI study applies DMAIC (Define, Measure, Analyze, Improve, Control) inside Lean Six Sigma as the project structure, with Value Stream Mapping and time-motion analysis as the diagnostic tools, and fuzzy logic to handle variability in operator decisions during changeover [S5].
For sourcing, the 2024-2026 dates cluster on practical guides (Tulip, Flowdit, First Resonance, EMI, MaintainX, EAS, Insite Packaging, Igus) and one peer-reviewed MDPI engineering proceedings paper; the consensus band for a conventional molding-line pattern swap without SMED is 30-90 minutes, and the consensus band after a SMED program is below 10 minutes for the stop-the-clock portion [S1][S2][S3][S4][S5][S6][S7][S8][S9].
Trackable signals over the next quarter: the next MDPI or SAE release on DMAIC + fuzzy-logic changeover work (a follow-on to the 2025 study), any new OEM release of pattern-preset HMI firmware on core-machine lines, and the next EAS or Insite field data point on realized percentage reduction in changeover minutes per installed SMED retrofit [S5][S7][S8][S9].
See also our earlier report, Steel-Plastic Composite Pipe for Commercial Buildings: Selection Criteria, Limits, and.