A servo drive TCO analysis must include hardware, integration, energy, maintenance, downtime, and end-of-life costs, because motor-drive energy can account for up to 97% of lifecycle TCO [S2].
The calculation applies to industrial robots, conveyors, machine tools, packaging lines, and intralogistics systems, where acquisition price covers only one part of the committed cost.
What Servo Drive TCO Measures
Servo drive TCO is the discounted sum of costs from specification through disposal, including the servo drive, servo motor, controller, feedback device, installation, operation, maintenance, downtime, and decommissioning. [S3]
A complete model separates acquisition, integration, operation, maintenance, and end-of-life expenditure. Industrial robot hardware typically represents 25–40% of the total investment needed for a functioning production cell, leaving 60–75% outside the robot arm itself [S3].
The comparison should use the same duty cycle, production volume, energy tariff, labor rate, discount rate, and service life for every candidate. Mixing manufacturer list prices with machine-level lifecycle costs produces a false result.
Hardware Price Drivers
Servo-system hardware pricing depends on motor torque, encoder resolution, thermal design, feedback type, protection rating, and control capability. Motors with the same frame size, voltage, and rated torque can differ by 40–200% in price [S4].
Volume tier changes the commercial basis of the quote. Local technical support, warranty coverage, stocking, and replacement compatibility can outweigh a nominal motor-price difference, so the request for quotation should state annual quantity, delivery schedule, and service coverage rather than unit price alone [S4].
Energy and Operating Cost
Energy use is the largest recurring cost in many motor-drive systems: one analysis places energy at up to 97% of motor-drive TCO over the lifecycle [S2]. Studies cited by Nidec Control Techniques indicate that energy consumption can account for up to 97% of a motor-drive system's total cost of ownership over its lifecycle [S2].
The energy model should calculate kWh at the motor terminal by multiplying average electrical power by annual operating hours, then adding demand charges, power-factor penalties, cooling demand, and any power that is recovered through regenerative braking. Energy-recovery functions can return braking energy in cranes, elevators, and extruders [S2].
That range supports a quantitative comparison with fixed-speed conveyor drives, but it should not be transferred to every machine without a duty-cycle check.
Integration and Commissioning Cost
Robot hardware typically represents 25–40% of the total investment required for a functioning production cell, while the remaining 60–75% lies outside the robot arm [S3].
Panel design, motor and encoder wiring, network infrastructure, controller setup, and cycle-time validation therefore belong in the servo drive budget, not under a miscellaneous installation allowance.
The related Servo Drive Spec Checklist provides the technical inputs needed to prevent value-engineering errors: current rating, voltage, encoder feedback type, duty cycle, and communications must be matched before comparing commercial offers.
Maintenance, Downtime, and Failure Exposure
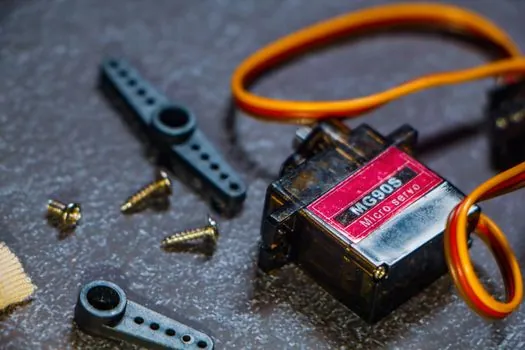
Servo-drive maintenance cost includes preventive inspections, cooling-system service, bearing and coupling checks, encoder condition monitoring, firmware management, spares, technician labor, and emergency dispatch.
Downtime must be valued by the affected asset, not by repair labor alone. A six-axis industrial robot might list for $50,000–$150,000 depending on payload and reach [S3].
A TCO model should therefore record the failure probability of the drive, motor, encoder, reducer, and feedback network, then multiply expected loss by lost contribution margin rather than adding the full sales value of every minute of downtime.
Servo Drive Options Compared
Selection criteria are operating value, motion performance, integration burden, and failure exposure, not motor sticker price. The comparison below shows where compact drives, standard industrial drives, and motion-controller-integrated systems fit. [S1]
This comparison is not suitable for a VFD specified solely for pumping, HVAC, or fan duty. A servo drive is justified where closed-loop positioning, torque control, coordinated motion, or fast deceleration has measurable production value.
Who Should Buy a Servo Drive
A servo drive is suitable for applications requiring controlled position, speed, or torque, especially robotic joints, CNC machines, packaging equipment, conveyors, and camera gimbals [S1]. Servo drives enable the high-speed, high-accuracy motion control required for automated storage and retrieval systems, conveyor sorters, AGVs, AMRs, and robotic picking arms [S5].
A servo drive is not the default choice for fixed-speed, continuous-duty equipment where variable-speed operation alone provides the required benefit. The stepper drive option can fit lower-cost positioning applications, while the AC motor route remains appropriate when precise closed-loop control is unnecessary.
For multi-axis robots, the servo press category applies only when controlled force and press-position behavior are required. A conventional motor and pump arrangement should remain the comparator if the process does not benefit from servo regulation.
Ownership Calculation and Procurement Decision
The purchasing decision should use net present value over a stated service life: acquisition plus integration plus energy plus maintenance plus downtime minus residual value. A practical bid comparison should also include commissioning hours, annual kWh, preventive-maintenance hours, expected failure cost, warranty coverage, local support, and the price of a stocked replacement drive [S4].
Acquisition and integration costs dominate the engineering work, while energy and downtime dominate the operating case in high-duty systems. The intralogistics servo-drive market, valued at USD 1.27 billion in 2026, is projected to reach USD 2.68 billion by 2035 at a 7.8% CAGR, confirming that lifecycle operating performance remains central to a competitive equipment decision [S5].
The next procurement checkpoint is a like-for-like TCO sheet with five verified inputs: motor continuous power, annual operating hours, electricity tariff, expected annual downtime, and installed commissioning labor. The Servo Motor TCO lifecycle decision guide can then be used to connect motor-side assumptions with the complete drive package.