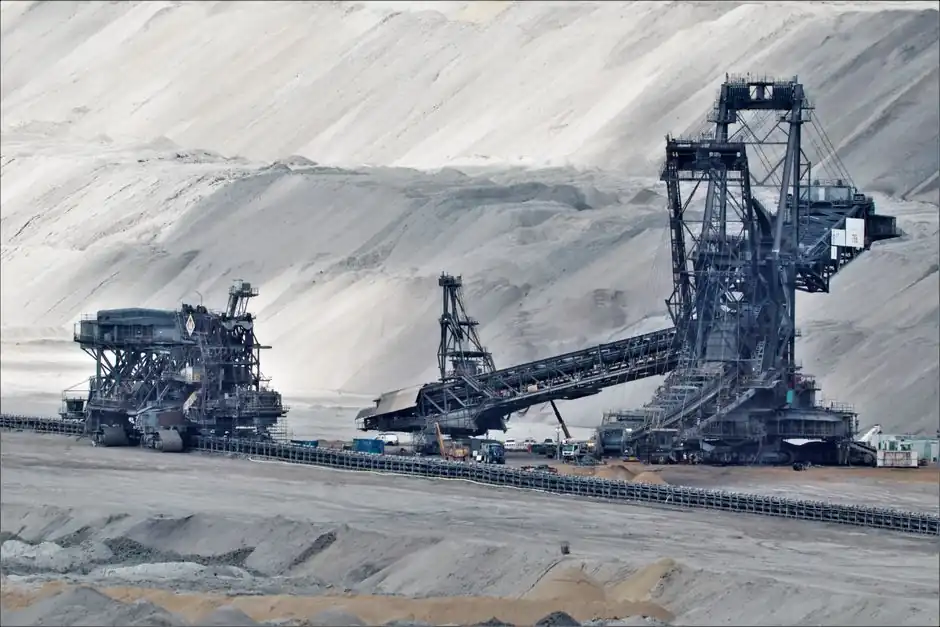
Bulk density, maximum lump size, and lift geometry are the three inputs that drive conveyor width, diameter, speed, and horsepower, and skipping any one of them is the most common cause of field failure. CEMA-based belt calculations, ISO 5048-derived national codes, and screw-conveyor engineering guides all key off the same triangle: how heavy the material is per unit volume, how big the largest particle is in any axis, and how high or how far the conveyor must move it [S2][S3][S5].
Each input has a defined engineering role. Bulk density converts volumetric throughput into mass flow (tons per hour or pounds per hour), lump size governs minimum belt width and minimum screw diameter, and lift sets the incline correction factor and the drive power budget [S3][S4][S5]. Designers who treat any of the three as optional typically see one of three predictable outcomes: chronic overload, plugging at the feed, or drive tripping on start-up under a fully loaded trough.
Bulk Density: The Mass-Flow Anchor
Bulk density is the weight of the loose bulk material per unit volume, usually expressed in lb/ft³, kg/m³, or t/m³, and is the only input that lets a designer convert a tonnage target into a required volumetric cross-section on the belt or in the screw trough [S2][S3]. Screw conveyor capacity is calculated volumetrically in ft³/hr and then multiplied by bulk density to confirm mass flow, so a 10% error in density propagates directly into a 10% error in conveyor diameter or speed [S3].
The same data point behaves differently across a screw conveyor versus a belt conveyor. A screw conveyor in a typical bulk-solids plant is sized at 15%, 30%, or 45% trough loading depending on the material, and a denser product needs less volume for the same mass flow, which is why the trough-loading value is paired with a specific bulk-density value in every published table [S3]. For belt conveyors, density enters the CEMA equation C = ρ × V × A, so a denser material lets the designer cut belt width or speed for the same tonnage, with industry practice commonly designing to about 85% of the theoretical cross-sectional area to absorb surge [S5].
The lab value is not always the operating value. Bulk density shifts with moisture, compaction in a silo, particle-size distribution, and aeration during feed, so the S2 guidance is to ask suppliers for a minimum and a maximum, then compare against what the plant actually handles on its weigh-feeder or load-cell data [S2]. IS 11592 (2000) builds its belt-width selection tables around the same density inputs, with belt widths of 300–2 000 mm as the codified range and up to 3 000 mm permitted when technical data is available [S4].
Lump Size: Belt Width and Screw Diameter Triggers
Lump size is defined as the maximum dimension of the largest lump in the bulk material, and when one axis of a lump is much longer than its transverse cross-section, the longer dimension is what governs the design [S1][S3][S7]. Steel grit is the textbook example: its lump size is the diameter of the grit, not its length [S1]. The definition is not a styling choice; it is the variable that drives minimum belt width on a troughed belt and minimum screw diameter on a flighted conveyor.
For belt conveyors, the width of the belt is predominantly governed by two factors: the lump size of the material conveyed and the capacity requirements [S4]. Troughed belt conveyors are explicitly used for higher capacity, higher speed, and for handling bulk material of large lump size, with the trough angle (commonly 20°, 35°, or 45° on three-roll idlers) setting how much of that lump the geometry can carry without spillage [S5][S6]. Lump size also sets skirtboard gaps, chute geometry, and the class of impact idler required at the loading zone [S5].
For screw conveyors, lump size is a hard diameter constraint, not a soft suggestion. The allowable size of a lump in a screw conveyor is a function of the radial clearance between the outside diameter of the center pipe and the inside radius of the trough, and the conveyor diameter must be increased whenever the lump-size distribution makes the standard diameter too tight [S3]. The character of the lump also matters: hard, non-degrading lumps demand a bigger screw than soft lumps that break up in flight, which is why bulk materials with easily broken-up lumps carry no limitation on conveyor size from a lump standpoint [S3].
Lift and Incline: The Geometry That Resets the Power Budget
Lift, expressed as the vertical rise of the conveyor, is the third input that has to be on the same datasheet as bulk density and lump size, because it changes the effective horsepower required to move the same mass flow. Every degree of incline above the design baseline multiplies into the drive power calculation, and the CEMA, ISO 5048, and DIN methods all carry an incline correction that is read off the same set of material inputs [S4][S5]. The vertical lift also determines whether a screw conveyor is even viable, since most screw conveyors are limited to inclines of about 20–45° depending on the material; beyond that, a different equipment class is required.
On a belt conveyor, the lift enters the calculation through the lift term of the CEMA drive equation, added to the horizontal motion power and the frictional losses on the idlers [S5]. When the same tonnage is run on an inclined belt at, for example, 18° instead of level, the drive power can rise by 30% or more before any material-property change is applied, which is why the same bulk density and lump size that works on a horizontal run can stall a drive on a steeply inclined one. Designers who change the layout without re-checking the lift term end up with tripped VFDs on ramp-up, especially under cold-start conditions.
The S2 screw-conveyor checklist captures the layout inputs that engineers consistently miss: conveyor length, incline angle, inlet and discharge locations, drive location, and whether the conveyor is control-fed or flood-fed [S2]. Flood feeding an inclined screw at start-up loads the trough before the drive can ramp, which is one of the most common reasons screw conveyors plug, overload the drive, or wear through couplings within the first weeks of service [S2]. Layout is not metadata; it sits on the same line of the datasheet as density and lump size.
Putting the Three Inputs Side by Side
Bulk density, lump size, and lift do not act on a conveyor independently, so the practical comparison is how each input changes the sizing decision against the same set of design criteria. [S2]
On belt width selection, bulk density is a soft driver (a denser material lets the designer trim width at fixed tonnage), lump size is a hard lower limit (belt width must accommodate the largest lump), and lift has a second-order effect through surcharge angle and edge retention [S4][S5]. On screw diameter selection, bulk density sets the volumetric-to-mass conversion, lump size sets a hard minimum, and lift sets an upper incline limit beyond which a different conveyor class is needed [S2][S3]. On drive power, bulk density is linear with mass flow, lift is approximately linear with vertical rise, and lump size acts indirectly through the diameter and speed that the lump constraint forces [S3][S5].
For a working spec sheet, the three inputs should always be carried in the same units the designer will calculate in: bulk density in lb/ft³ or kg/m³, lump size as a single largest dimension in mm or inches, and lift as both the horizontal length and the vertical rise in the same units, plus the resulting incline angle in degrees [S2][S5]. If any of the three is missing, the calculation should be treated as preliminary only, and the supplier or in-house engineer should be told which value is assumed so the resulting margin can be checked [S2].
Common Failure Modes From Missing or Wrong Inputs
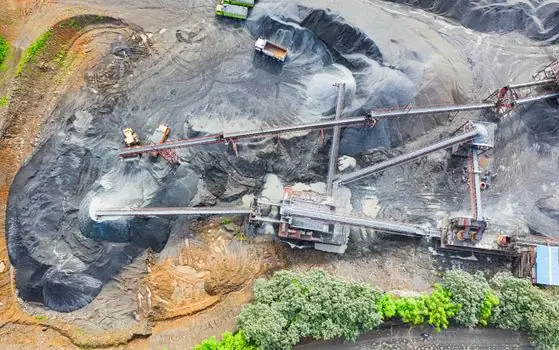
When bulk density is assumed low and the plant actually handles a heavier grade of the same product, the conveyor moves the right volume per hour but is overloaded by mass, with the usual signature being drive tripping, belt slip on the drive pulley, and accelerated idler bearing wear. When lump size is understated, the largest particles bridge at the skirtboard or lodge in the screw flight, producing impact damage on the belt cover, broken cleats, and screws that stall against a lodged lump [S3][S5].
When lift is added to an existing conveyor without resizing the drive, the VFD or soft-starter trips on ramp because the motor cannot develop the additional torque under a fully loaded trough, and a redesign of the drive package becomes the only safe fix [S2][S5]. The S2 piece is explicit on this point: a screw conveyor can hit its target throughput and still be the wrong conveyor for the job, and the most common reason is that critical application information, including lift, was missing during sizing [S2]. For industrial systems engineering context, see this write-up on how PLC scan time caps machine throughput and what to do about it, which covers the control-side limits that compound any conveyor-sizing error.
Sourcing and Standards Discipline
For belt conveyors, the dominant calculation frameworks are CEMA (North America) and ISO 5048 with national derivatives, including IS 11592 (2000) for India, which covers belt widths of 300–2 000 mm and is reaffirmed through the 2010 amendment [S4]. The CEMA 7th Edition is the current reference for belt-conveyor methodology, with CEMA targeting about ±10% accuracy under conventional inputs and about 3% running sag as a design target [S5]. DIN and ISO/DIN methods are widely used in European practice and produce comparable answers when the input values are realistic [S5].
For screw conveyors, the CEMA 300/352 series and manufacturer engineering guides (KWS, Martin, Rulmeca, Flexicon) publish bulk-material tables with bulk density, material factor, and recommended component series for each commodity, and these tables should be the starting point for any new sizing [S3]. Material names on a spec sheet should be specific (grade, moisture, particle size), not generic, because flour, sludge, ash, and plastic can each span a wide range of conveying behavior within a single category [S2]. For adjacent equipment standards work, see the spec breakdown of DIN EN 16983 disc spring groups, which is a useful reference for how European codes group tolerance bands.
Operational signals worth tracking: published updates to the CEMA 7th Edition tables, any new edition of IS 11592 or ISO 5048, and conveyor OEM engineering guides refreshed in 2025 or 2026, since these are the documents a sizing engineer cites when the spec is challenged in commissioning [S4][S5]. The verifiable next node is a side-by-side review of the CEMA and ISO 5048 power calculations on a single worked example, which would let a process engineer confirm that the chosen method matches the available input data.
The underlying component specifications are covered under bulk bag, and vertical lift module.