Apparel distribution checkweighers run at 100-300 packages per minute on polybagged or boxed garment sets, with required accuracy of ±1-2 g for individual items and ±5 g for multi-piece bundles, using EMFR or strain gauge load cells matched to throughput and tolerance targets [S3][S8].
The use case is completeness verification on hanging, folded, or boxed apparel packs going into retail and e-commerce fulfilment, where the checkweigher replaces manual spot-checks and immediately detects missing shirts, trousers, or accessories in a kit [S8]. Production lines in this segment typically handle package weights from 50 g (a single folded T-shirt polybag) up to 10-20 kg (a case of mixed apparel), and the equipment must integrate with conveyors, sortation, and WMS/ERP data capture [S2][S7].
Checkweigher architecture and load cell options
A checkweigher is built from a feeder, precision scale, line divider, discharge unit, and a computerized control system, with accuracy and stability determined primarily by the load cell technology inside the scale module [S1][S2].
For apparel work, two load cell families dominate. Electromagnetic force restoration (EMFR) cells deliver ±0.1 g typical accuracy on packages up to 6 kg, with low drift over temperature and time, and are the right pick for premium labels, multi-piece kits, or compliance-driven e-commerce where each missing SKU is a return event [S3]. Strain gauge cells sit at ±0.5-2 g depending on capacity, are cost-effective, and are widely used on lighter apparel SKUs from 50 g to a few kilograms, provided a routine calibration schedule is in place [S3]. Selection should be driven by the smallest acceptable giveaway on the heaviest single SKU and the largest reject zone you can tolerate statistically.
Throughput, accuracy, and reject mechanism trade-offs
Modern checkweighers cover 60 to 600+ packages per minute with measurement accuracy of ±0.1 g to ±5 g depending on weight range and line speed, so the spec sheet must be matched to the actual conveyor pitch and product length, not the brochure maximum [S3].
For a 100-300 ppm apparel line, dynamic accuracy of ±1-2 g is achievable with both EMFR and quality strain gauge systems, but only if the weighing zone is sized to the longest garment pack and the conveyor vibration is isolated. Reject mechanism choice matters as much as load cell choice. Pneumatic pushers handle up to 200 ppm and are common in apparel because they tolerate variable polybag sizes; air blast suits lightweight bagged items; drop-through and diverter conveyors are reserved for heavier boxed apparel or case-pack checks [S3]. For a structured comparison across decision criteria, the table below lines up the main configurations an apparel DC will see on quotation:
Configuration comparison for apparel distribution: (1) Compact strain gauge checkweigher, 50 g to 6 kg range, ±1-2 g dynamic accuracy, up to 200 ppm, pusher reject, lowest cost, suits single-piece polybagged garments. (2) EMFR checkweigher, 50 g to 6 kg range, ±0.1-0.5 g dynamic accuracy, up to 300 ppm, pusher or air blast, mid-to-high cost, suits premium multi-piece kits. (3) High-load case checkweigher, up to 120 kg, ±5-20 g accuracy, lower ppm, chain transport with timing, suits end-of-line carton and multipack completeness [S2][S3].
Standards, compliance, and audit documentation
Look for manufacturers operating under ISO 9001 quality systems, with equipment designed to OIML R76 for non-automatic and automatic weighing instruments, and check whether the supplier documents GMP and HACCP alignment where apparel and personal-care items are packed in shared facilities [S2][S4].
Connectivity also needs early specification, since apparel DCs typically run RS232, Ethernet, or Profibus to WMS and ERP layers, and the same applies to high-load case scales used at end-of-line [S2]. For audit readiness, demand logged weight records per package, statistical process control charts, and a documented calibration interval. A pre-purchase audit of the manufacturer's quality system, after-sales support, and spare-parts lead time is a stronger predictor of long uptime than headline accuracy alone [S4].
Apparel-specific integration considerations
Apparel checkweighers typically run on a hanging-garment conveyor or a belt conveyor downstream of polybagging, where the line is shared between single-piece items, multi-packs, and full cartons, and one weighing station has to handle all three without re-tooling [S8].
Weight control systems on textile and clothing lines detect missing items by verifying that a declared set of garments hits a specified total weight, which both raises customer satisfaction and reduces returns on incomplete orders [S8]. In practice this means the OEM must supply recipe management per SKU, with target weight, upper and lower limits, and reject class stored against the SKU barcode, and a checkweigher that can switch recipes on the fly as bag sizes change over a shift. For broader handling context, the spec reality check for vibrating conveyor selection in apparel distribution shows why conveyor isolation, not just the scale head, often decides whether a checkweigher holds its rated accuracy in a live DC.
Who this equipment is for, and where it falls short
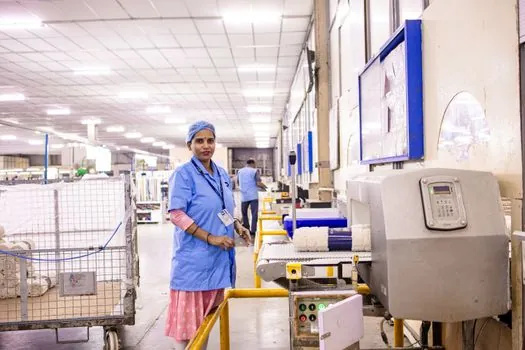
Inline checkweighers are the right call for apparel DCs running above 60 ppm on uniform polybagged or boxed SKUs, where each missing item is a return cost, and where the operator base can support routine calibration and recipe management. [S2]
They are the wrong tool for low-mix, low-volume fulfilment under 30 ppm, where manual spot-checks remain cheaper, and for hanging-garment flows where pack geometry varies so much that a stable weighing window cannot be maintained. They also fall short where upstream bagging has high inherent weight variability, since a ±5 g checkweigher cannot rescue a ±15 g filling process. For a fuller handling-side spec map, the chain conveyor selection for air cargo piece flow reference covers high-load case weighing integration on the same kind of chain transport used in 120 kg class scales.
Sourcing and due diligence on the manufacturer
Selection criteria on the manufacturer side mirror the technical criteria: documented quality system, customization range on capacity, software, and reject mechanism, regional technical support with defined response time, and a published spare-parts and after-sales program [S4].
Reputation and sector experience are not soft factors. A vendor with installed apparel and textile references will already understand polybag static, hanging-garment swing, and the WMS integration pattern, which shortens commissioning from months to weeks. Independent confirmation of accuracy claims under live line conditions, not just at the OEM demo hall, is the single most important pre-purchase test before signing a purchase order [S4].
Track the published revision of OIML R76 and any update to weights-and-measures rules in your shipping destinations before locking the spec, since legal-for-trade resale by weight remains rare in apparel but completeness-check claims still need a defensible calibration chain. Watch also for 2026-2027 product launches from the major packaging inspection OEMs that target the e-commerce polybag segment with lower-cost EMFR heads, which will reset the price-to-accuracy curve for mid-tier DCs.
Detailed specification references: checkweigher, distribution cabinet, and power distribution.